At H&C, we pride ourselves on the partnerships we develop through helpful insights into providing our customers better products, processes, and productivity. Our consulting solutions are based on decades of experience in the field.
Customer-Focused Services
Five ways we keep your floor running
These case studies only briefly touch the surface of our deep expertise, but they’ll no doubt touch on challenges you face at your own operation. Every one follows the same discipline: define the problem, test the fix on the customer’s own machine, and measure the result.
Case Study
Kennametal End Mill Test
The Client
Contract manufacturer of machined components in Western N.Y.
The Challenge
Shorten the cycle time of a roughing operation, improve tool life, and increase throughput.
The Solution
H&C's representative recommended a 1-inch diameter Kennametal Harvi 2 five-flute end mill with a 43-degree flute angle and ALTIN PVD coating (KC643M grade). The tool runs with coolant and excels in steel, cast iron, stainless steels, and titanium.
The Benefit
Roughing process reduced from 45 minutes to 2.6 minutes
Spindle speed increased from 1,700 RPM to 2,670 RPM
Feed increased from 3.5 IPM to 60 IPM
SFM increased from 450 to 700
Passes reduced from 2 to 1
End mills purchased per year cut from 34 to 17
288 hours of scheduled machine time saved per year
45 min → 2.6 min
Roughing cycle time
2×
End mill life
288 hrs
Machine time saved / year
Case Study
Kennametal Tap Test
The Client
A local contract manufacturer tapping blind holes in 17-4PH stainless steel.
The Challenge
Poor productivity and tap life on a blind-hole tapping job using a high-speed steel OSG 10-32 2B tap with an oxide-coated surface.
The Solution
H&C recommended testing a Kennametal tap with a chromium carbide carbon (CRCC) coating. Kennametal technicians came to the customer's facility and ran the test on their machine, on their parts.
The Benefit
Speeds and feeds more than doubled
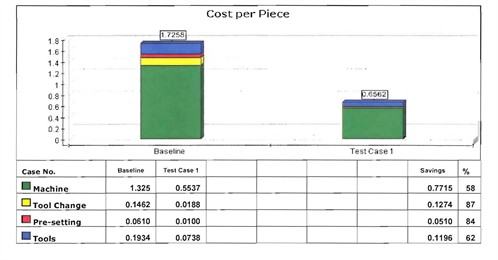
Tapping cycle reduced from 1.06 minutes to 0.443 minutes
Tap life increased from 164 holes per tap to 1,000 holes per tap
Tap usage on this job dropped from 25 taps per year to 4
Cost per piece dropped from $1.73 to $0.66
24 hours of machine time freed per year
164 → 1,000
Holes per tap
$1.73 → $0.66
Cost per piece
2×+
Speeds and feeds
Case Study
Increase Tool Life, Decrease Expense
The Client
An Upstate New York contract machining company working with copper.
The Challenge
Drills were loading with chips and breaking while creating threads. Taps were tearing threads and, at times, breaking too.
The Solution
An H&C application engineer suggested coating select tools with CRN to reduce edge buildup, then ran testing to prove out the new tooling before the customer committed.
The Benefit
Significant improvement in the quality of pre-tapped holes and threads
5-to-1 tool life increase with drills
8-to-1 tool life increase with taps
Overall reduction in machine time and tooling costs, with a measurable productivity gain
The material was causing burrs at the intersections of the thread crest. The customer had already tried inserts from multiple manufacturers without the results they wanted.
The Solution
An H&C application engineer visited the shop, reviewed the process and tooling in person, and concluded that a Kennametal top cresting LT style of insert would solve the problem.
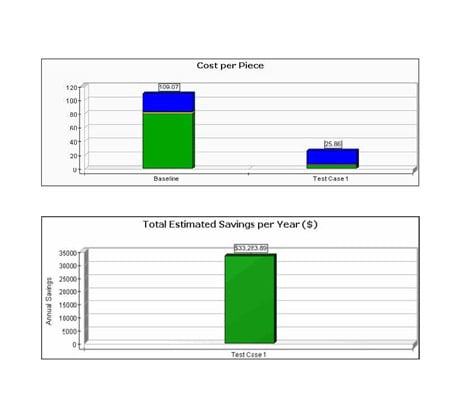
H&C ran Kennametal’s Beyond Grades KCP10 and KCP25 in a roughing and finishing application against a major competitor at a CNC machining and manufacturing plant out of Oneida, NY. The result: tool life tripled, and the customer realized an annual cost savings of $27,000.
Head-to-head testing
Same machine, same material, same operator. Only the tooling changes.
Measured, not estimated
Tool life tracked across real production runs, not lab conditions.
Cost math included
Every study translates tool life into annual dollars saved.
Want a test like this on your floor?
Visit our special requests and promotions page for a quick response to requests for quotes, or to try a tool such as an insert, drill, mill, or grinding wheel.